Smältblåst tyg är att använda höghastighets hetluftsflöde för att dra den tunna strömmen av polymersmälta som extruderas från munstyckshålet på munstycket, och därigenom bilda ultrafina fibrer och samla dem på nätgardinen eller rullen, och samtidigt binda sig själva till att bli smältblåst non-woven-tyg.
The meltblown fabric widths of regular manufacturers are generally 1600mm, 2400mm, 3200mm, and the extruder diameters are usually 90mm, 105mm, 135mm. However, after the epidemic began, the small computers (that is, the ones used by the Yangzhong family workshop) were small in width, usually only tens of centimeters, and the screw diameters were mostly 45mm, 50mm, and 65mm.
Denna typ av maskin har låg effekt och låg kvalitet, men kostnaden är billig och leveranstiden är snabb. Priset före epidemin var bara 20 000 till 20 000, men nu har det stigit till 200 000, men det är fortfarande mycket billigare än vanliga tillverkares extruder. För närvarande ärmaskin för smältblåst tygfrån vanliga 1600 vanliga tillverkare på marknaden säljer för mer än 6 miljoner yuan, och leveranstiden är mer än 2 månader.
Produktionsprocessen för smältblåst duk är huvudsakligen följande:
1. Smältberedning
2. Filtrera
3. Mätning
4. Smältan extruderas från öppningen
5. Smält trickle drawing och kylning
6. in i nätet
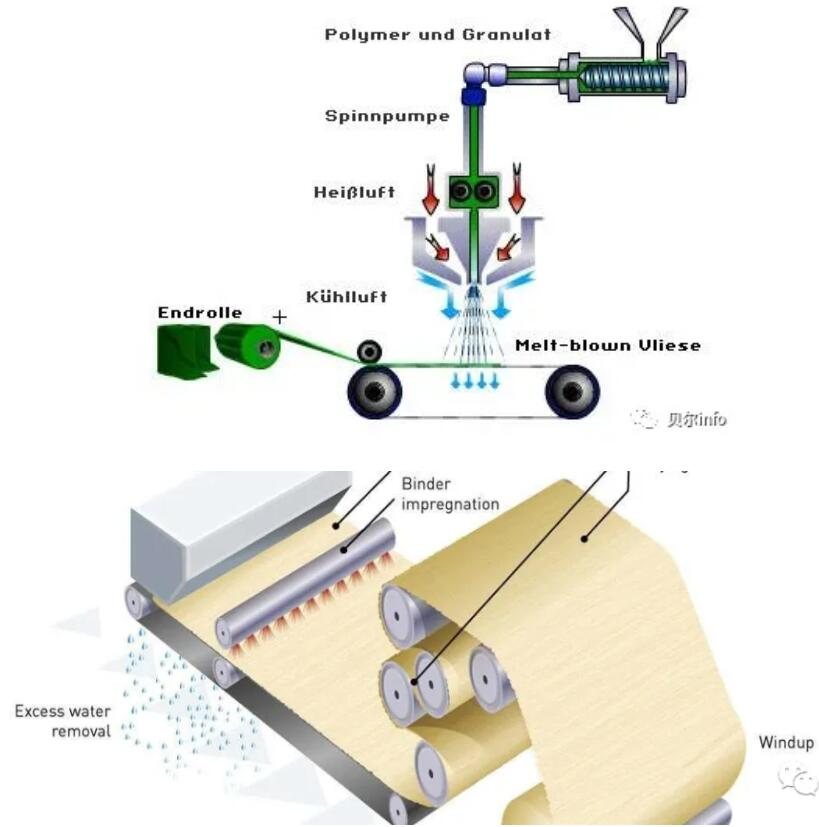
Översikt och princip för smältblåst tygutrustning
Smältblåsning är en metod som förlitar sig på hög temperatur och höghastighetsluftflöde för att blåsa polymersmältan så att den snabbt kan sträckas för att preparera fibrer.
Efter att polymerspånen har värmts upp och trycksatts av en skruvextruder till smält tillstånd når de spinndysshålet vid munstyckets främre ände genom smältfördelningskanalen och sträcks sedan av två konvergerande höghastighets- och högtemperaturluftflöden för att göra dem tunna.
Den förtunnade fibern kyls och stelnar på nätanordningen för att bilda ett smältblåst non-woven-tyg.
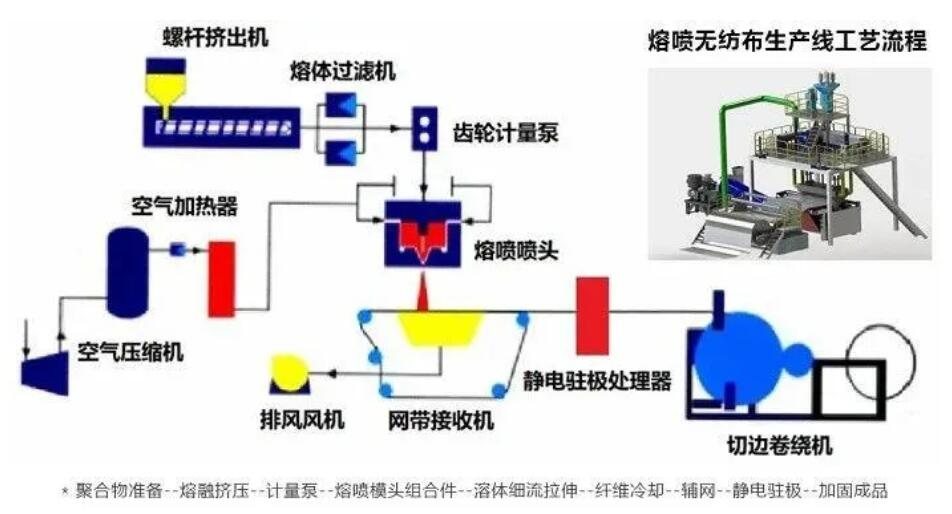
Komponenter i utrustning för smältblåst tyg
Nyckelutrustning såsom smältblåst huvud, komponenter för automatisk laddningssystem, ultraljudsrengöringsmaskin, luftvärmare, centrifugalfläkt, skruvextruder, smältblåst banformningsmaskin, smältblåst offline lindningsmaskin, smältblåst offline slitsmaskin.
Kärnkomponenten i smältblåst tygutrustning --- spinndysa
The spinneret for melt spinning is a representative spinneret for the manufacture of synthetic fibers such as polyester and nylon. The thermoplastic resin is heated and melted, and it is extruded through the spinneret in air or water at a certain speed and cooled. Spinning method that solidifies into fibers.
The core technology is the small nozzle on the spinneret. This nozzle is not only small in size, only 0.15mm, but also has a complex hole pattern on such a small nozzle, which is extremely difficult to process, and the nozzle processing process requires Several months. If the processing accuracy is not high, the final meltblown cloth produced will not meet the corresponding technical requirements, which will affect the protective performance of the mask.
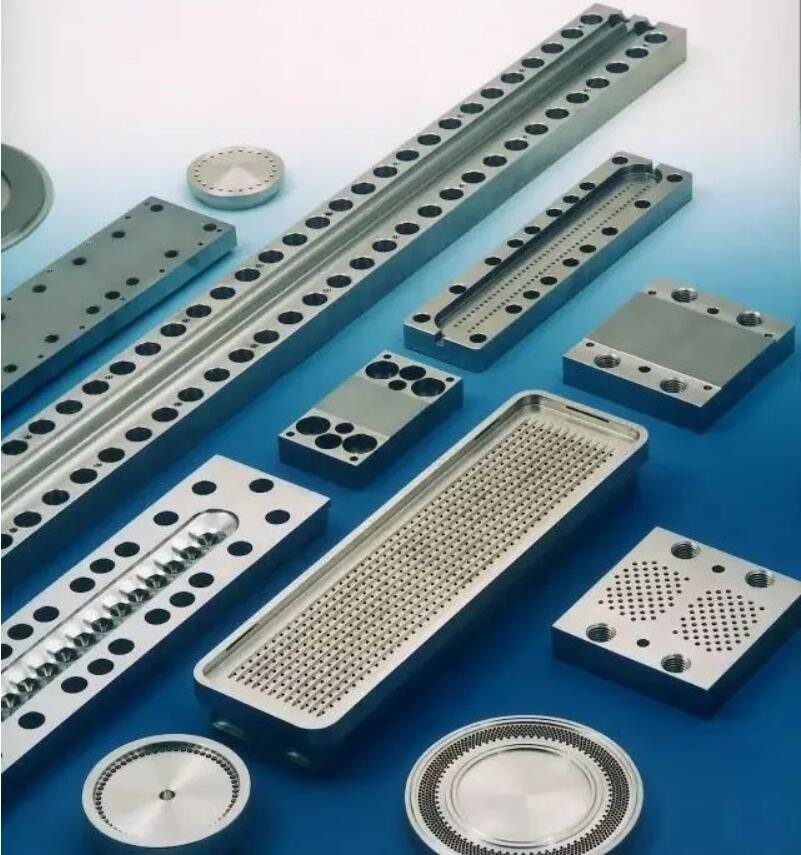
Struktur av smältblåst tyg spinndysa
The structure of the spinneret is divided into three forms according to the shape of the spinneret, round, fan and rectangular. At present, circular plates and rectangular plates are used more at home and abroad. In order to be suitable for different kinds of chemical fiber spinning occasions, round spinnerets are divided into flat plate type, flange plate type, plate ring, flange ring, etc.: rectangular spinneret is divided into flange rectangle and flange groove rectangle, etc. , It is mostly used for short fiber spinning with more holes.
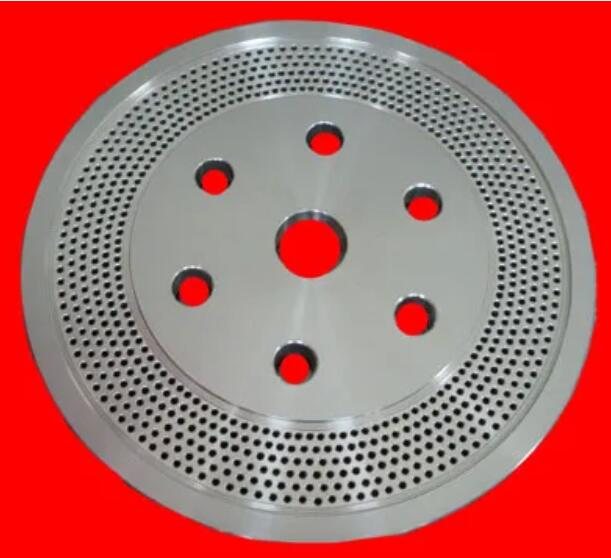
Smältblåst tyg spinndysa struktur
Smältblåst formhuvud
The die head includes a die head main body, a spinneret and an air plate. The spinneret and the air plate are detachably installed in the die head body. There is a spinneret hole in the spinneret, and there are several gaps between the spinneret and the air plate. There are several gas circulation channels in the main body of the die head, and the gas circulation channels are connected with the gap groove. The outer wall of the die head body is provided with a gas pipe connection end, which is connected to the gas collection cavity through a gas pipe Through, one end of the spinneret hole of the spinneret is fixedly connected with an interval flow stabilizing piece, and the other end of the spinneret is fixedly connected with a pipe connection device.
Spinnmunstyckets hål är anslutet till utloppsporten på skruvextrudern genom röranslutningsanordningen Ansluten.
In meltblown equipment, meltblown die is one of the core components to realize high polymer wire drawing. The design and accuracy directly affect the length, uniformity, toughness, fineness and many other aspects of the wire drawing, thereby affecting the quality of the final coil. Have a decisive impact.
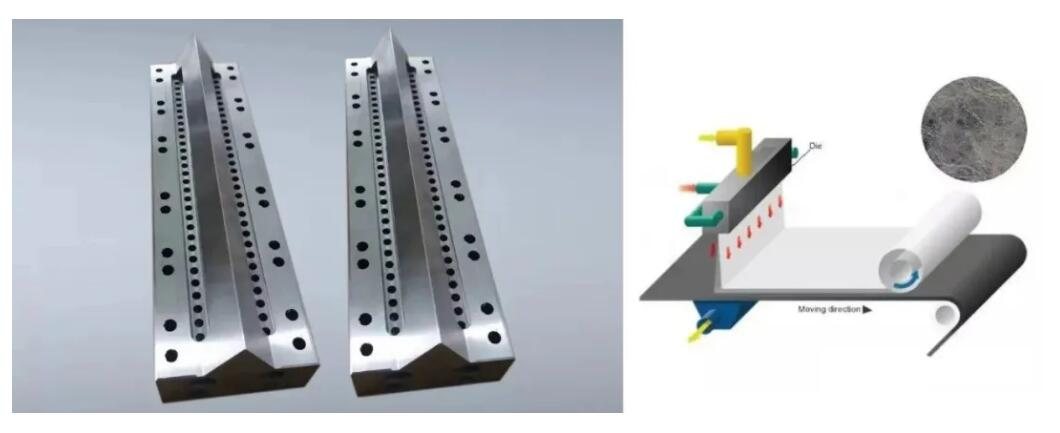
Smältblåst formhuvudstruktur
Smältblåst luftvärmare
That is, the pipeline heater is composed of a body and a control system. The heating element is made of stainless steel pipe as a protective sleeve, high temperature resistance alloy wire, crystalline magnesium oxide powder, formed by a compression process, and the control part adopts advanced digital circuits and integrated circuit triggers. , High back pressure thyristor and other components constitute an adjustable temperature measurement and constant temperature system to ensure the normal operation of the electric heater.
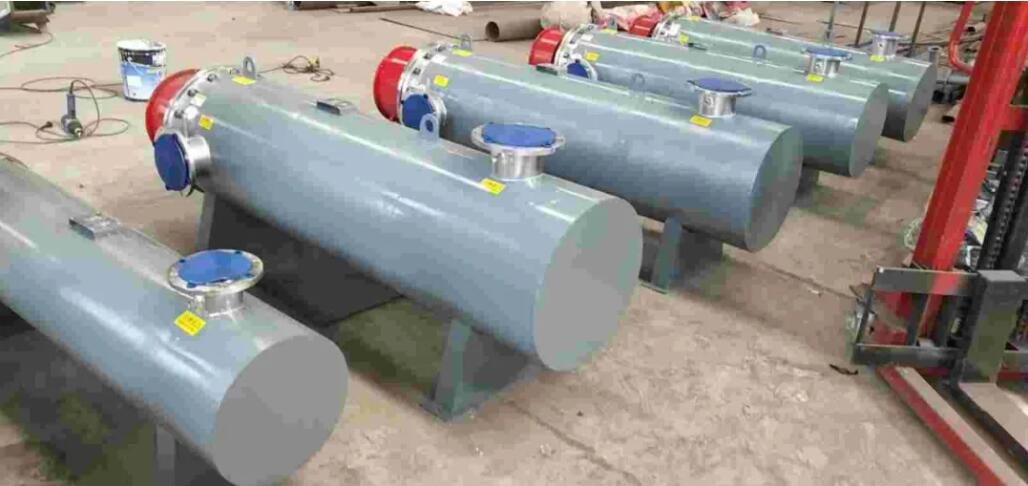
Smältblåst luftvärmare
Polypropylene materials are extracted from petroleum. Currently, Sinopec and other companies can produce them in large quantities, but the equipment that produces polypropylene as melt blown cloth, especially the core components and spinnerets, mainly depends on imports. These suppliers mainly include Japan's Kasen spinneret, German Enka, and Japanese spinneret. Japanese suppliers occupy the most important position. With the current output of several companies, it is far from satisfying the market demand.
Therefore, the production capacity of masks ultimately depends on the output of the melt blown cloth production equipment, and the core spinneret nozzle of the melt blown cloth production equipment is very difficult to produce. The processing time takes several months, and the output cannot be greatly increased in a short time. And the production capacity is very limited, which also makes the mask production can only maximize the use of current equipment and increase production by extending the working time of the production line.
Huvudenhetskonfiguration
1. Skruvextruder; 2. Doseringspump; 3. Smältblåsningsanordning; 4. Mottagningsnät; 5. Lindningsanordning; 6. Matningsanordning.
Utrustningen i den kontinuerliga produktionslinjen av smältblåsta nonwovens är cirka 6 m hög, 5 m bred och 20 m lång. Produktionsutrustningen är som följer:
(1) Skruvextruder: Skruvdiametern är i allmänhet 100~120 mm och förhållandet längd/diameter är 30. Syftet är att smälta skivorna.
(2) Mätpump: Dess funktion är att noggrant mäta, kontrollera uteffekten och fiberns finhet. Det är en kugghjulspump som kontinuerligt levererar smältan till spinndysan.
(3) Smältfilter: Dess funktion är att filtrera bort föroreningar i smältan för att undvika att täppa till spinndysens hål.
(4) Transportnätsgardin: Den smältblåsta fibern tas emot jämnt och sprids på nätet och transporteras framåt. Det finns en sugfläkt under den för att släppa ut den varma luften som kommer ner från toppen.
(5) Spinning box: It is the key equipment of the melt-blown process. There is a strip-shaped spinneret, which is covered with a long row of spinneret holes. Generally, there are about 1500 nozzle holes per m. The two sides of the spinneret are equipped with hot air nozzles, and there are hot air nozzles underneath, which form an angle of 50b with the nozzle holes. After the fiber is ejected, the high-speed hot air is used to stretch the air flow immediately to blow the fiber and become superfine fiber.
(6) Matningssystem: Det består av 3 mättrattar, som används för att mäta vita skivor, masterbatch och tillsatser. De 3 komponenterna går in i blandaren nedan för att blanda jämnt och sätts sedan i produktion.
(7) Varmluftsfläkt och värmare: tillhandahåller temperaturen och trycket för den varma luften som används i den roterande luftflödesritningen, använd el för att värma och förbrukar mycket ström.
(8) The coiling machine adopts automatic coiling, and the melt blown cloth is packaged in rolls. Meltblown nonwovens are characterized by ultra-fine fibers, and the smallest fiber diameter can reach 0.5Lm, generally between 1~5Lm. The finer the fiber, the better the quality of meltblown cloth, but the output is relatively reduced. Because the fiber is ultra-fine, its specific surface area is large, and the adsorption capacity is strong, which is the most prominent advantage of melt blown cloth.
Om du är intresserad av maskiner för tillverkning av smältblåst tyg kan du besöka länken för mer information och videodemo nedan:https://www.troysupply.com/1200-1600mm-width-melt-blown-fabric-machine_p130.html
Stort tack från TROY!