


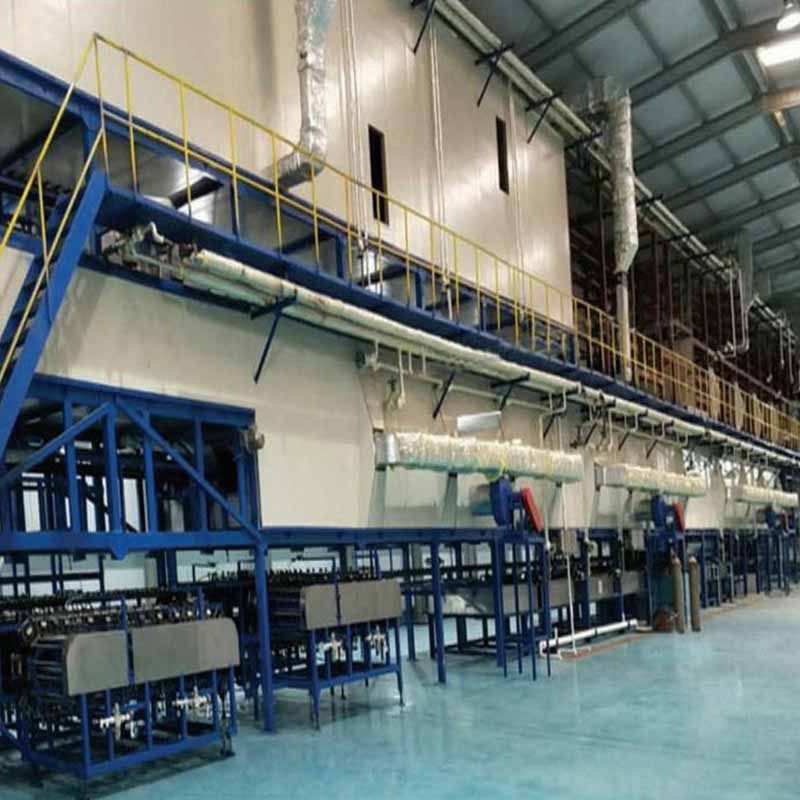
Maszyna do produkcji rękawic nitrylowych
TR-SBB to system automatyzacji pakowania/napełniania. Kluczowe dane techniczne: Główne produkty Rękawice z PVC/lateksu/winylu. Czas realizacji wynosi 60 dni; cena podana jest za konfigurację. Certyfikaty: Dokumentacja CE na życzenie.
- Model
- TR-SBB
- Główne produkty
- Rękawiczki z PVC/lateksu/winylu
- Kategoria
- Sprzęt automatyki
- Czas realizacji
- 60 dni
Do czego służy ta platforma
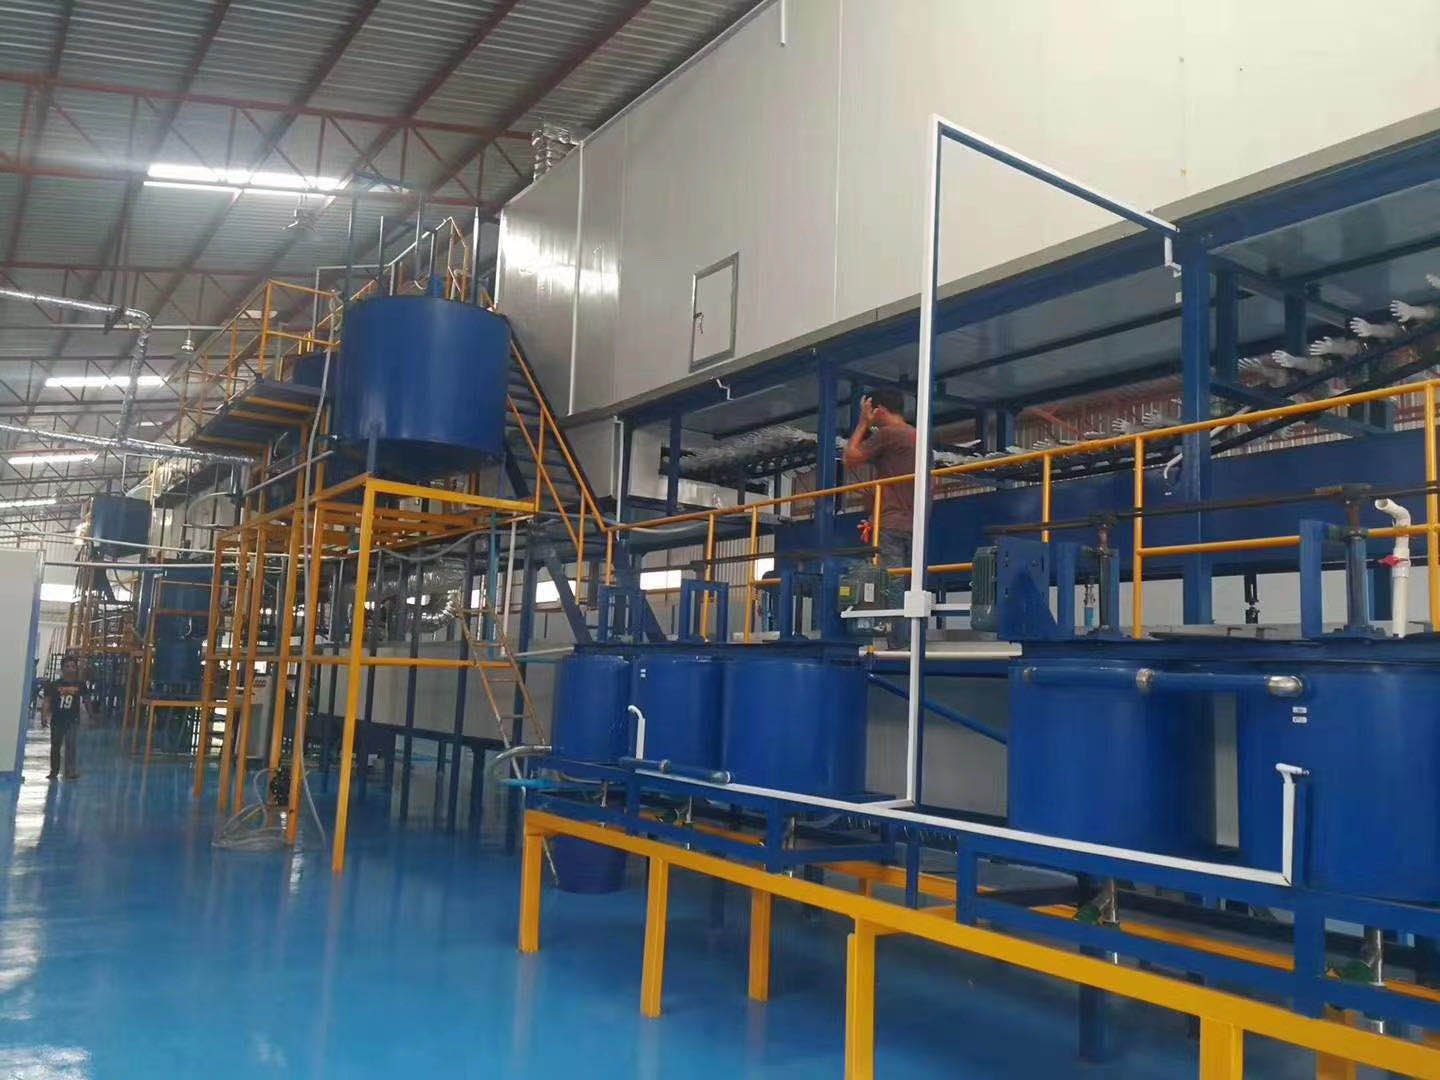
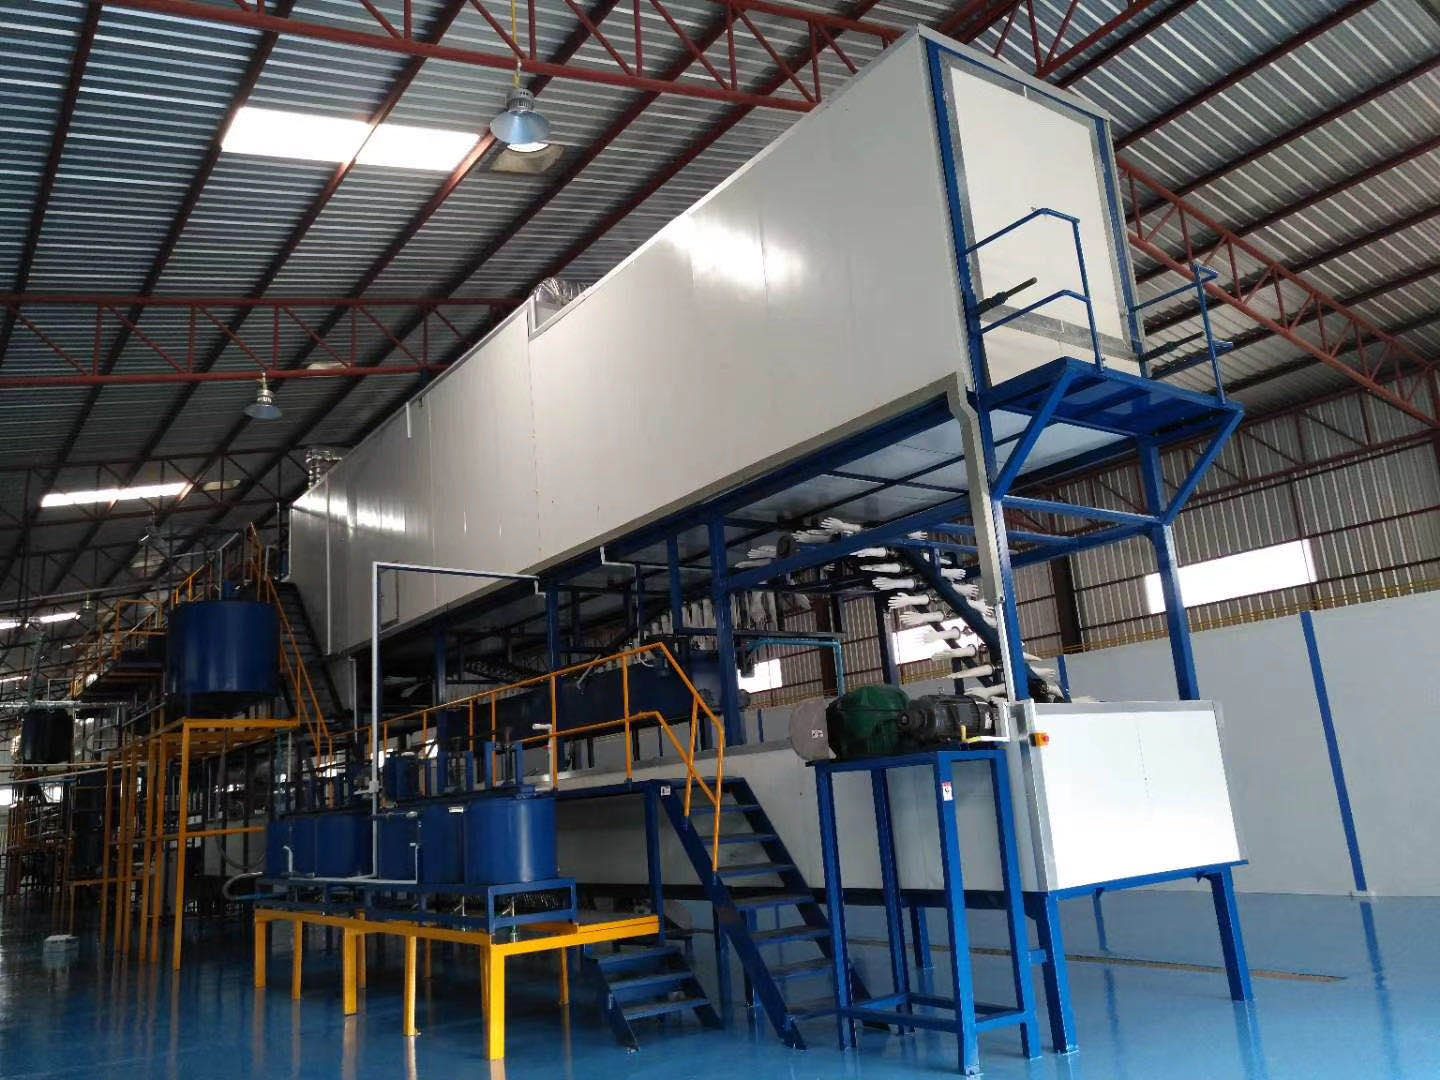
Automatyczna linia do produkcji rękawic nitrylowych produkuje rękawice z PVC/lateksu/winylu do kontroli i chirurgii, jednorazowe rękawiczki domowe. Oszczędność energii, niska awaryjność. Znajdź szczegółowe informacje na temat maszyny do produkcji rękawic nitrylowych.
Warunki handlowe
| Cytat | Cena za konfigurację — odpowiedź w ciągu 48 godzin |
|---|---|
| Czas realizacji | 60 dni |
| MOQ | 1 jednostka |
| Pochodzenie | Chiny |
| Port załadunku | Shanghai, China |
| Incoterm | FOB Shanghai / CIF on request |
| Zapłata | 30% depozytu, 70% przed wysyłką |
| Gwarancja | Standardowo 24 miesiące, opcjonalnie 36 miesięcy |
Szczegóły produktu
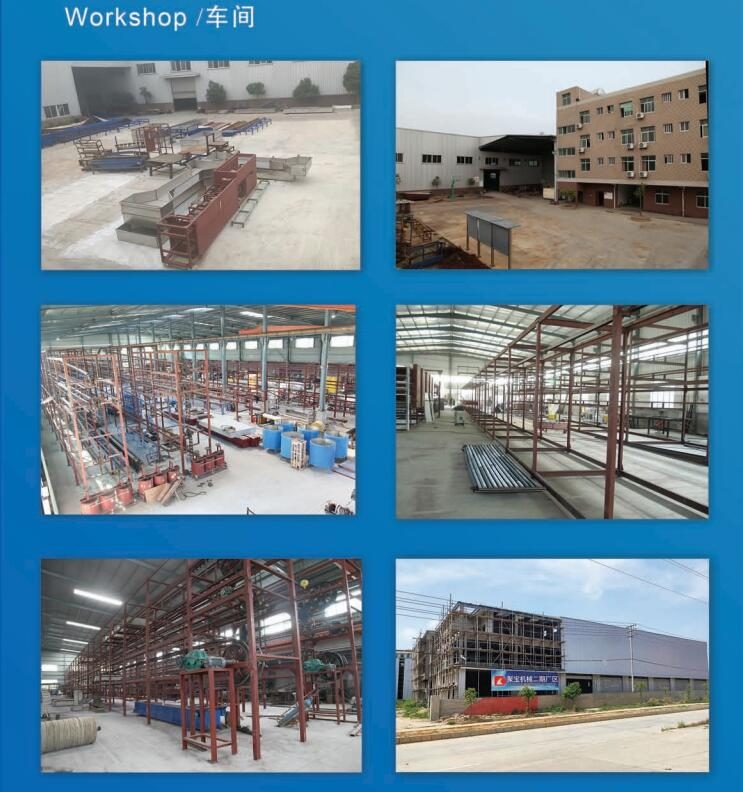
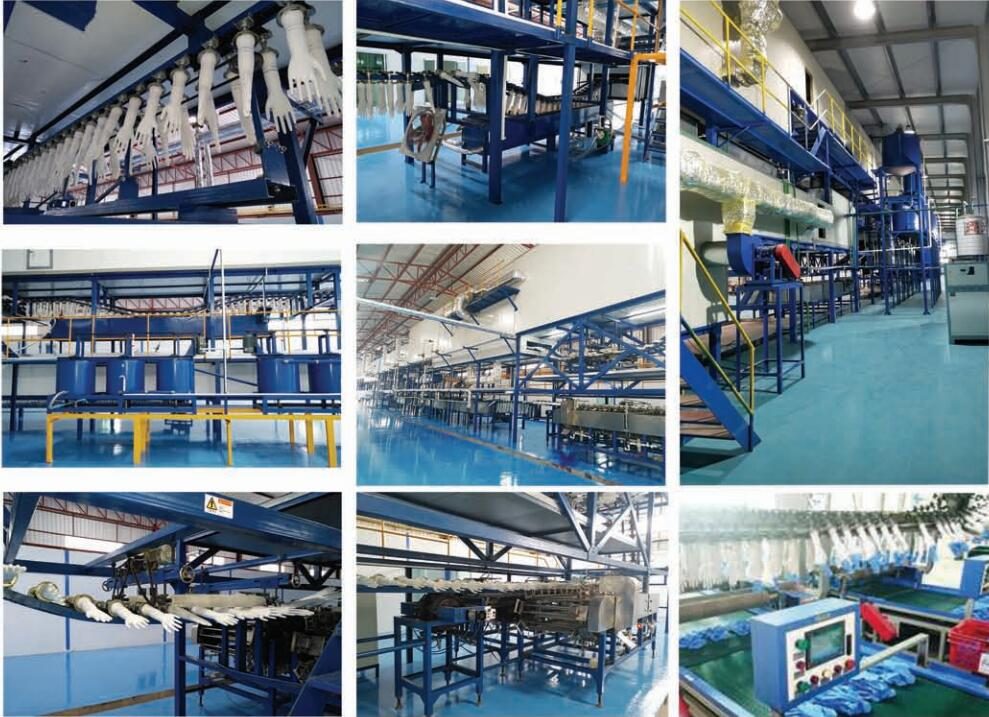
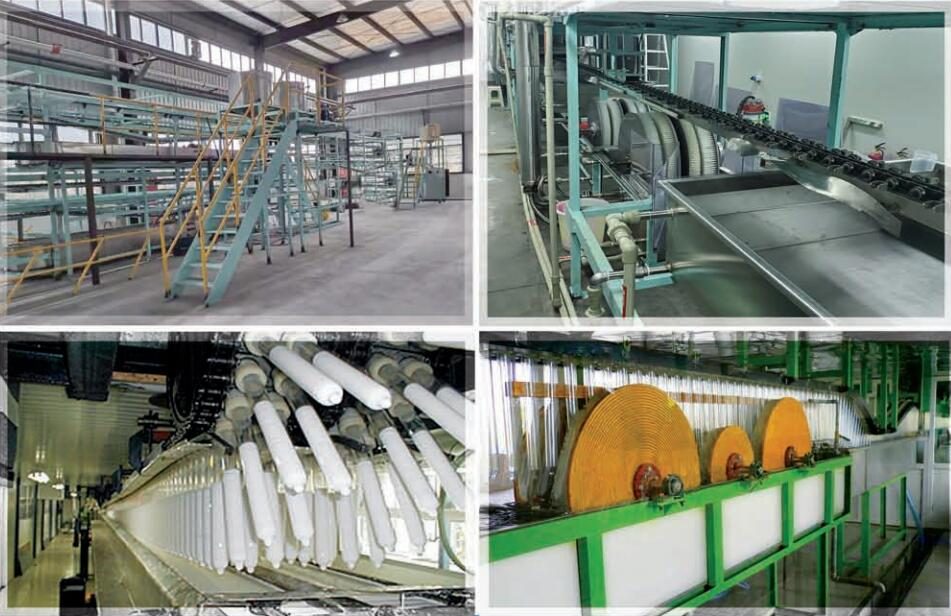
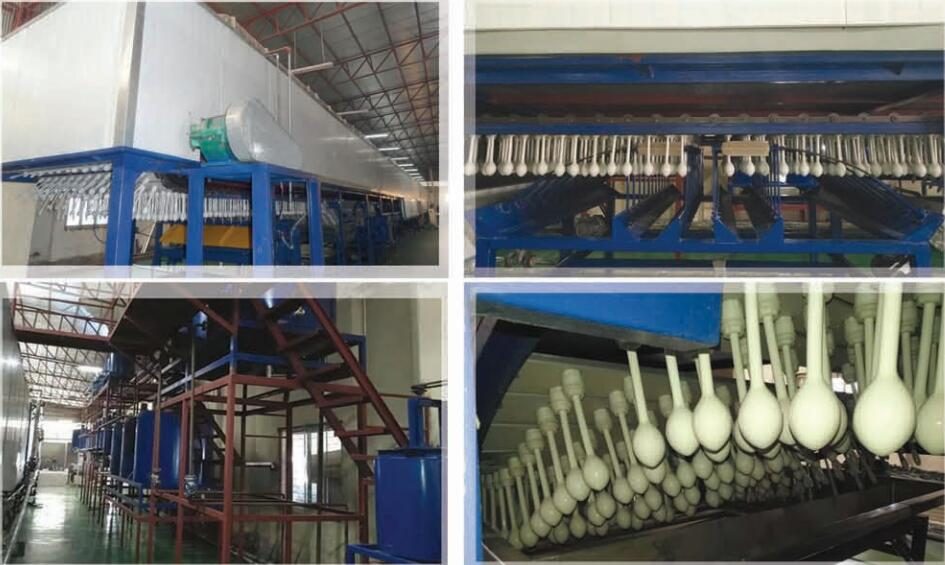
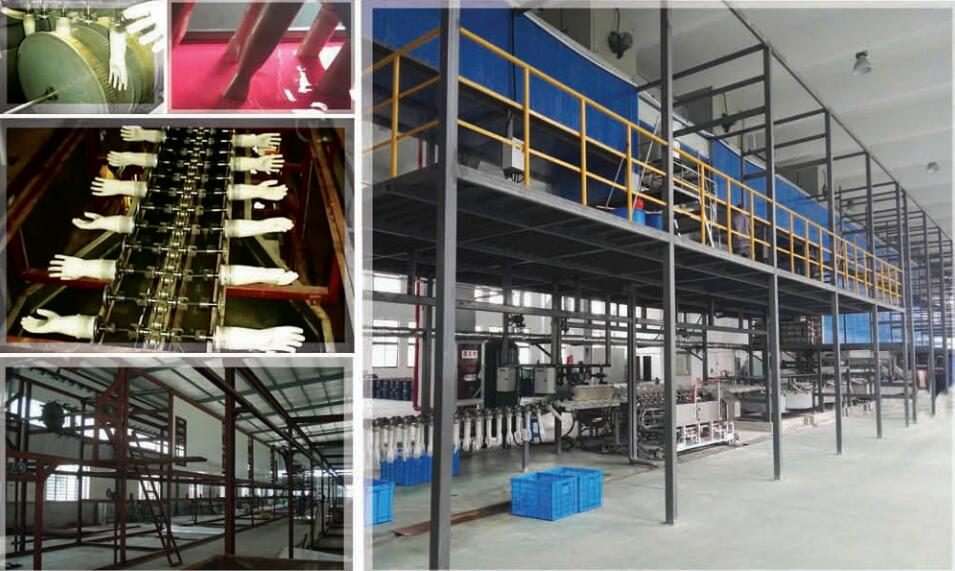
Noty aplikacyjne, rysunki konstrukcyjne i wideo z dokumentacji inżynierskiej TROY – ta sama dokumentacja dostarczona wraz z ofertą.
| AUTOMATIC GLOVE DIPPING LINE SPECIFICATION | ||
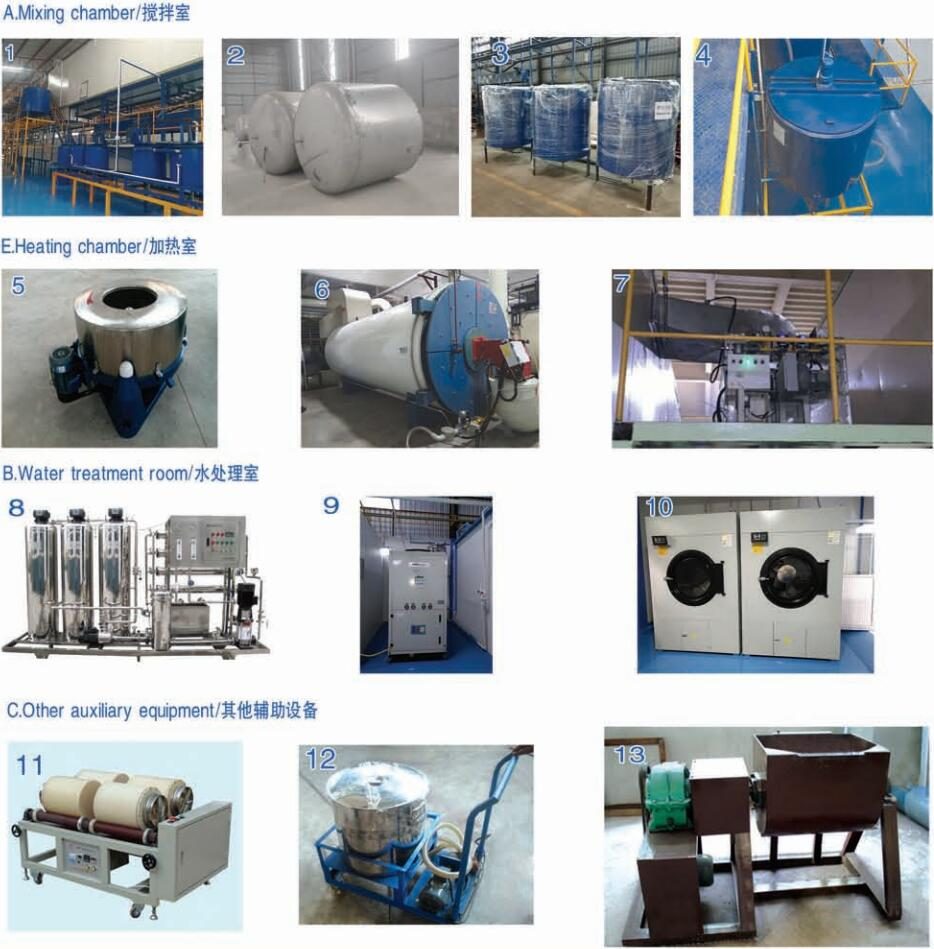
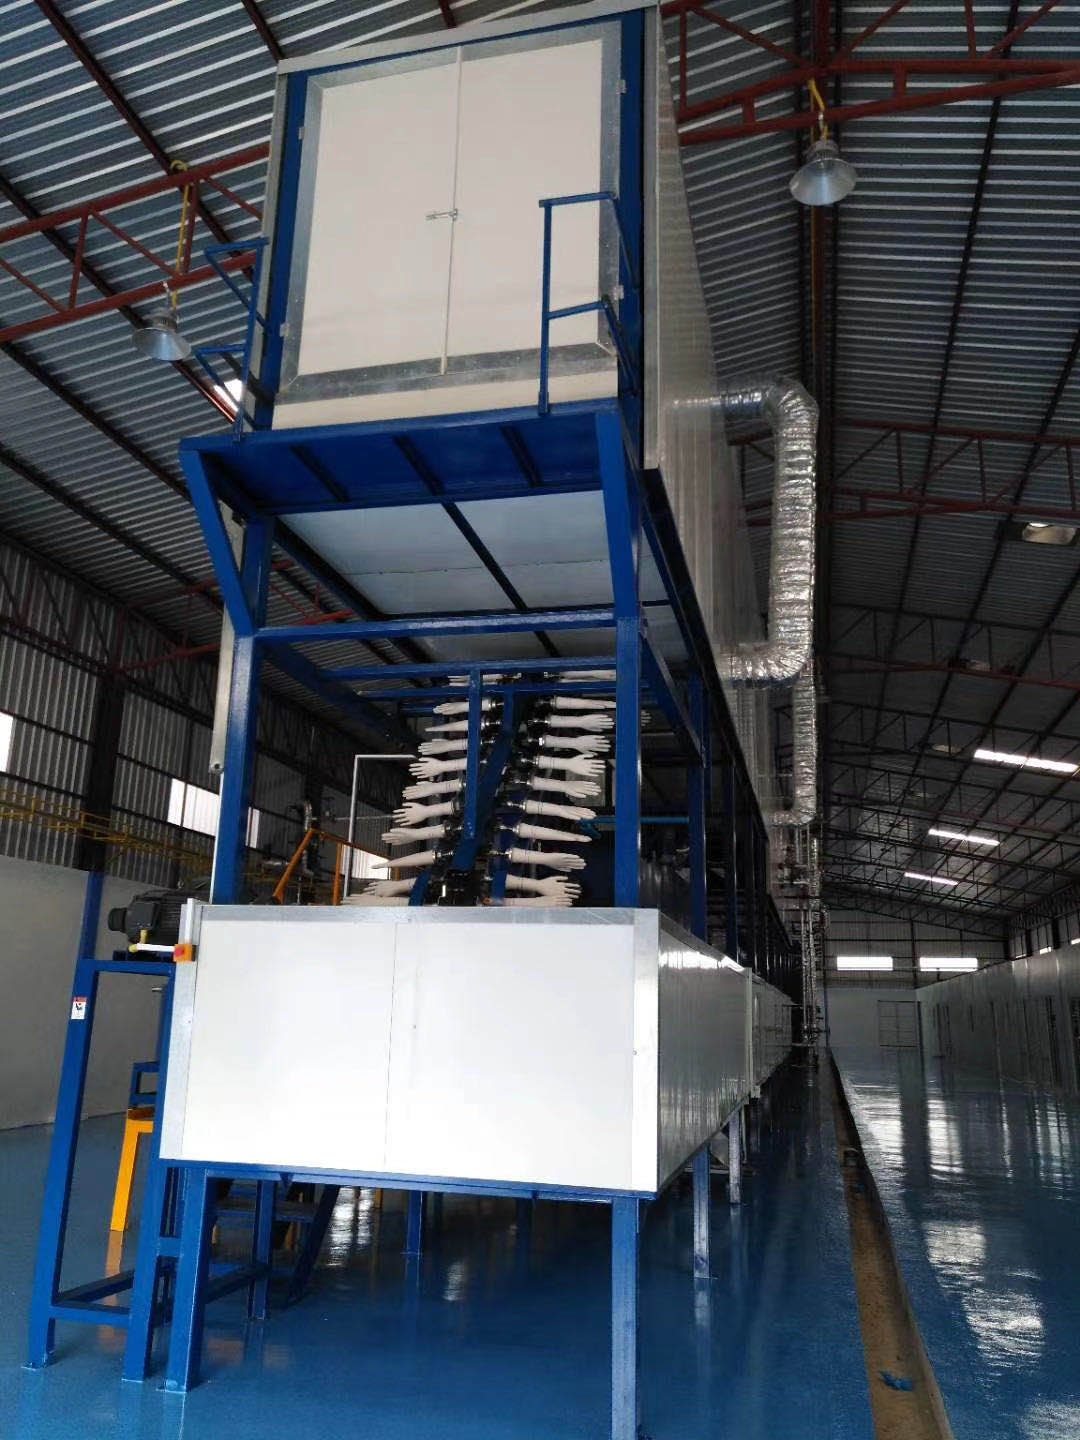
| 1 | Type Of Chain | Chain is the life of the Gloves production line, every processes of the production line is drive by the chain,and connecting the entire process flow, different production lines using different drive chain, we use 100mm pitch chain relative to the various types of tracks, the main purpose is to reduce the wear and tear of the transmission process, noise and smooth travel. And use gravity to tension the system to make sure the chain is tight at all times. |
| 2 | Frame material and technical requirements | Structural requirements of the main is solid combination of high-carbon steel : 12 # square steel, 12# U-Steel,The main frame of the beam structure use of high carbon steel type 10*6 square pipe and 12 # channel.The main track also uses high-strength, wear-resistant high-carbon steel materials: 5 # U-shaped steel, 12 # C steel and other supporting the production line as the main transmission track use.The overall frame after the completion of the protective process, first coated with a layer of anti-rust paint to prevent rust corrosion of steel, and then coated with a layer of smooth finish, one is to strengthen the protective effect of the second is to make the machine look beautiful, depending on the process used Temperature resistant at 150-200 degrees Celsius temperature paint (according to customer requirements use top coat). |
| 3 | Napęd główny i pomocnicze urządzenia napędowe | Main drive of various production lines is driven by25KW motor and flange helical gears. The motor should be 3C standard. Because this motor is not easy to be hot, it can work effectively for a long time. The combination of the flange helical gear drive makes the main drive more smooth. Auxiliary drive equipment: mold brushing system, coagulant circulation system, sulfide mixture (latex, nitrile rubber, etc.) mixing system, starch circulation system, heat transmission distribution system, angle rotationsystem and other auxiliary production processes. |
| 4 | Zbiornik koagulantu, specyfikacja zbiornika z tworzywa sztucznego oraz wymagania techniczne i funkcje: | ①: The structure of the coagulant tank and the latex tank is composed of a groove body formed by double layers of materials inside and outside, a coagulant groove, and an outer layer of the glue groove is made of ahigh-carbon steel plate. The strong steel plate is favorable for keeping the shape of the groove body not to be deformed and the structural combination relatively firm . The inner use of 3mm 304 stainless steel, stainless steel has a uniform effect of heat and corrosion, the heat effect is significantly conducive coagulant, latex in the tank thermostat effect. |
| ②: Wkładka ze stali nierdzewnej 3mmt 304, główne ogrzewanie równomiernie i efekt antykorozyjny Zewnętrzna płyta pęcherzyka żółciowego o grubości 4 mm ze stali wysokowęglowej, główna konstrukcja nie jest stabilna odkształcenie. | ||
| ③: Coagulant tank, plastic tank with circulation mixing system, motor drive and stainless steel vane circulation pump composed of glue circulation system, the motor is not easy to hot long-term operation can be effective to the coagulant tank, plastic tank brought The stability of the cycle, and stainless steel leaf circulation pump anti-corrosion effect is good, easy to wear, will not give coagulant, glue caused by metal powder. | ||
| 5 | Specyfikacja i funkcja sprzętu do czyszczenia form: 2Acid tanks, 2 Alkali tanks, 2 hot water tanks | ①: Mold cleaning equipment which is a mould cleaning mechanism consists of pickling tank,alkaline cleaning tank, washing mould round brush and brush and a two heated water trough , these grooves use monolayer that made of 3mm sus304 stainless steel to heat directly tanks .However, round brush and transverse brush are made of engineering plastic board and nylon plate. The capacity of each groove makes in accordance with the requirements of the process. |
| ②: Each groove of the system has each function,the pickling tank is to clean residue on the mold, but alkaline cleaning tank is to clean up and counteract acid water on the mold and then enter washing and cleaning mode to make cleanliness of mold achieve initial effect, and finally two hot water troughs soak in water and wash dust of mould and make mould cleaner. | ||
| ③: Rura ze stali nierdzewnej SUS304 służy do wytwarzania wężownicy grzewczej podczas ogrzewania, a wężownicę umieszcza się bezpośrednio na dnie zbiornika w celu podgrzania płynu czyszczącego za pomocą odprowadzania ciepła ze ścian, aby uzyskać najlepszy efekt stałej temperatury. | ||
| 6 | Struktura funkcji zbiorników ługowniczych 3 leaching tanks +3 leaching tanks | ①: Zbiornik ługujący to termostatyczna kwadratowa szczelina oddzielona dwuwarstwowymi płytami. Użyj stali nierdzewnej 304 o grubości 3 mm, która ma dobry wpływ na akumulację ciepła i zapobieganie korozji. |
| ②: W zależności od różnicy w procesie zbiornik do ługowania będzie miał kształt kwadratowego rowka. Jego główną rolą jest pomoc w wycieraniu substancji białkowej z produktów i efekt podgrzewania. | ||
| ③: Większość podwójnych rowków całej linii produkcyjnej jest wbudowana w wężownicę grzejną z rurki ze stali nierdzewnej SUS304, a woda w warstwie pośredniej jest podgrzewana przez ściankę wężownicy, a następnie temperatura cieczy w zbiorniku jest kontrolowana na podstawie temperatury wody. | ||
| 7 | Budowa i funkcja rowków skrobiowych | ①: Rowek skrobiowy to zbiornik jednowarstwowy z funkcją mieszania obiegowego, wykonany ze stali nierdzewnej SUS304 o grubości 3 mm |
| ②: Zgodnie z różnicą w procesie, zbiornik skrobi, jego podstawową rolą jest pomaganie powierzchni produktu w przyczepianiu izolowanego proszku w celu uzyskania gotowych produktów po rozebraniu, a nie połączonych ze sobą | ||
| ③: Zbiornik skrobi polega na tym, że wężownicę rurową umieszcza się na dnie zbiornika w celu bezpośredniego ogrzewania | ||
| 8 | Crimping,flanging and automatic mold unloading system | ①: System curlingu składa się z różnych komponentów i mechanicznych zasad działania. |
| ②: System kołnierzy jest stosunkowo prosty. Jego funkcją jest wspomaganie systemu usuwania wlewków w maszynie striptizerskiej na początku pracy. Jest ona podobna do funkcji zaciskania, a ich materiałem jest okrągły trzonek szczotki wykonany z nylonu. | ||
| ③: The most complex process is automatic ingot stripping system in the whole production equipment, according to the processes and products are different ,so the structures of ingot stripping are different, the form of contact with the product release clip, splint, roller,circular brush shaft and other high-pressure air of ingot stripping mold and so on, and the materials used are also varied.Its main function is to reduce the human input, high working efficiency ,increasing output and so on. | ||
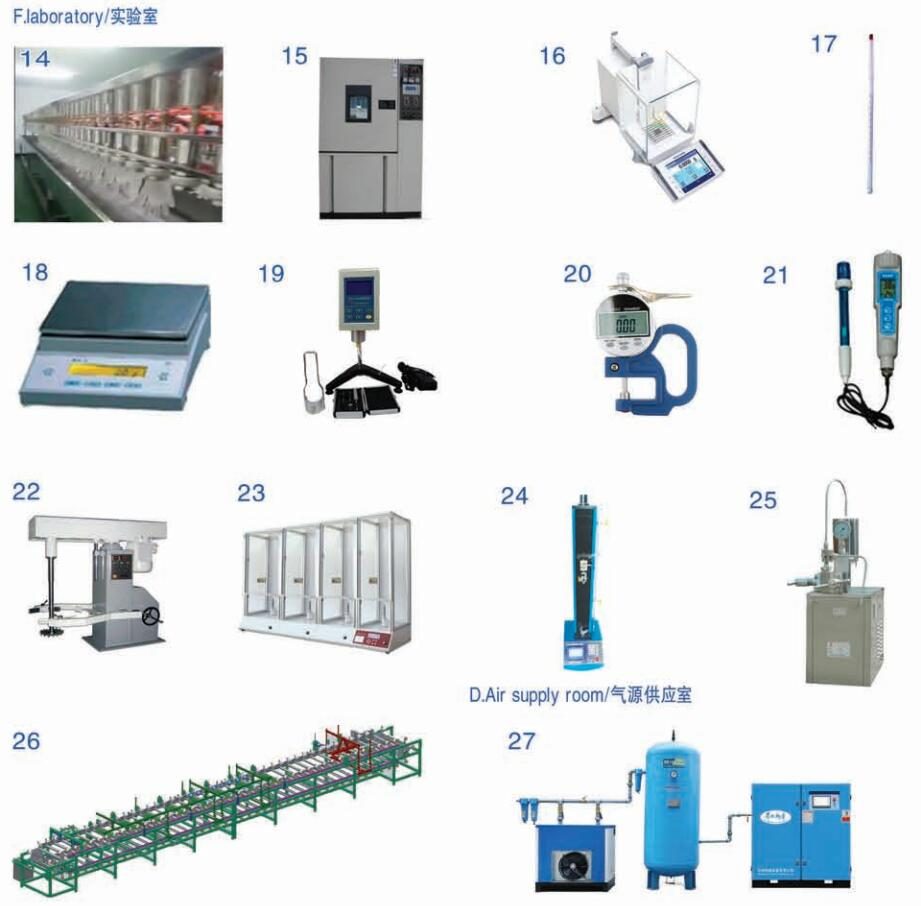
| 9 | Chemical Auxiliary Equipment | ①: Chemical process auxiliary equipment, mainly used for chemical grinding, blending, vulcanization and production added and so on,The chemical process is made of diaphragm pump, ball mill, sand mill, vulcanization mixing tank, storage tank, feeding tank, coagulant mixing tank, polymer mixing tank and powder tank.Different products in the production line using different chemical process auxiliary equipment for chemical production and use. |
| ②: Ball mill and sand mill is mainly used to grind chemical granule material,grinding it into fine powder,Ball mill to carry ceramic ball mill tank,use of a ceramic tank to scrolling on ball mill to grind chemicals,The sand mill is the use of agitation grinding chemicals,According to the needs of different processes to support. | ||
| ③: Vulcanization mixing tank, storage tank, polymer mixing tank, coagulant mixing tank, starch mixing tank, mixing tank and feeding tank are mainly used for mixing and adjusting the finished product directly to produce chemical materials. Rely on the mixing evenly chemical materials and prevent precipitation.according to the needs of different processes supporting. | ||
| ④: Chemical auxiliary tank is mostly use double constant temperature tank,the inner of tank using 3 mm 304 stainless steel plate which has heat evenly and anti-corrosion effect,The outer tank use a high carbon steel plate of 4mm, High-strength steel plate structure to play a solid and not easily deformed effect. | ||
| ⑤: System mieszania wykorzystuje cykloidalny silnik igłowy i sterowanie falownikiem, zgodnie z wymaganiami procesów chemicznych w celu zmiany prędkości mieszania, mieszając ostrza wykonane ze śrubowego mieszadła ze stali nierdzewnej TISCO 304. | ||
| 10 | Oven insulation board specifications and technical parameters details: | ①: Oven is combination of insulation board formed to be several independent oven, according to the process requirements to be different oven size, and the function of the oven is to provide heat of the heat collection space and the product heating and drying, the working temperature by the different artwork there are 80 -110, 110-130, 130-150, 150-170 ℃ |
| ②: Piekarnik z dobrym efektem izolacji termicznej i możliwością pracy w wysokich temperaturach wytrzymuje temperaturę 250-300 stopni Celsjusza, izolacja antresoli, solidność bawełny, gęstość bardzo dobra, dobre dopasowanie pomiędzy płytami, aby uniknąć wycieku ciepła, zmniejszając w ten sposób straty ciepła | ||
| ③: Materiał wewnętrzny Płyta ze stali nierdzewnej 0,6 mm SUS304, główną funkcją jest zapobieganie korozji i zwiększanie wytrzymałości płyty wewnętrznej. Zewnętrzny materiał płyty to płyta ze stali wysokowęglowej o grubości 1,0 mm, wzmacniająca cały gruby stopień płyty izolacyjnej. Bawełna izolowana warstwowo to bawełna skalna o grubości 78 mm, gęstość wynosi 130 kg/m3, może skutecznie uzyskać efekt izolacji. | ||
| 11 | Oven thermal equipment and dehumidification exhaust system: | ①: Ovens main thermal equipment are electric rods, infrared and fluid (oil, steam, hot air) heat pipe, radiator. Wind structure formed in the oven, the use of fan transmission distribution of heat while the moisture in the oven is discharged from the oven, the top of the oven every 10 meters has a 20mmX40mm Vapor evaporation gate hole to help deal with moisture, Keep the oven dry and reduce corrosion caused by moisture. |
| 12 | Control box Function | Klucz USB, przewodnik może mieć wyraźny obraz działania i może automatycznie obliczyć pojemność, zużycie i wygenerować raport. Safe alarm, malfunction diagnose |
| 13 | Electrical control box brand | Electrical control box |
| Air switch: South Korea-LS | ||
| Contactor:South Korea -LS | ||
| Electric relay: Japan - OMRON | ||
| Frequency control: Taiwan Delta | ||
| PLC computer programming integrated circuit control: Taiwan Delta | ||
| 10.4 inch color touch screen controller: Taiwan Weinview | ||
| Switching power supply: Taiwan - Mean well | ||
| Cylinder: Taiwan -AIRTAC | ||
Pełne dane techniczne
| Model | TR-SBB |
|---|---|
| Główne produkty | Rękawiczki z PVC/lateksu/winylu |
| Kategoria | Sprzęt automatyki |
| Czas realizacji | 60 dni |
Wartości są nominalne w temperaturze 20°C. Pobierz arkusz danych modeli CAD, krzywych momentu obrotowego i map we/wy sterownika.
Gdzie biegnie
Zwymiarowane i zlecone przez inżynierów TROY.
Zwymiarowane i zlecone przez inżynierów TROY.
Zwymiarowane i zlecone przez inżynierów TROY.
Zwymiarowane i zlecone przez inżynierów TROY.
Pytania kupującego
Jakie są kluczowe specyfikacje TR-SBB?
Główne produkty: Rękawiczki PCV/lateksowe/winylowe. Pełny arkusz danych jest dostępny na żądanie.
Jaki jest czas realizacji i MOQ dla TR-SBB?
Czas realizacji wynosi 60 dni; MOQ to 1 jednostka.
Jaka jest cena TR-SBB?
Ceny podane są dla każdej konfiguracji, łącznie z oprzyrządowaniem i transportem, jeśli ma to zastosowanie.
Uzyskaj ofertę cenową na TR-SBB
Uwzględnij część, dawkę docelową i port docelowy. Inżynier — a nie chatbot — odpowiada w ciągu 48 godzin.
Ta sama kategoria
Czterokolorowa maszyna do napełniania kremów
Uniwersalny automatyczny system podawania ślimaka i moduł dokręcający
Automatyczna maszyna do robienia bułek TRB-140
Oceniony przez TROY Engineering ·. Specyfikacje są ponownie sprawdzane z arkuszem danych dostawcy przy każdej ofercie.